info@mixfoodgroup.com
86 15221870316

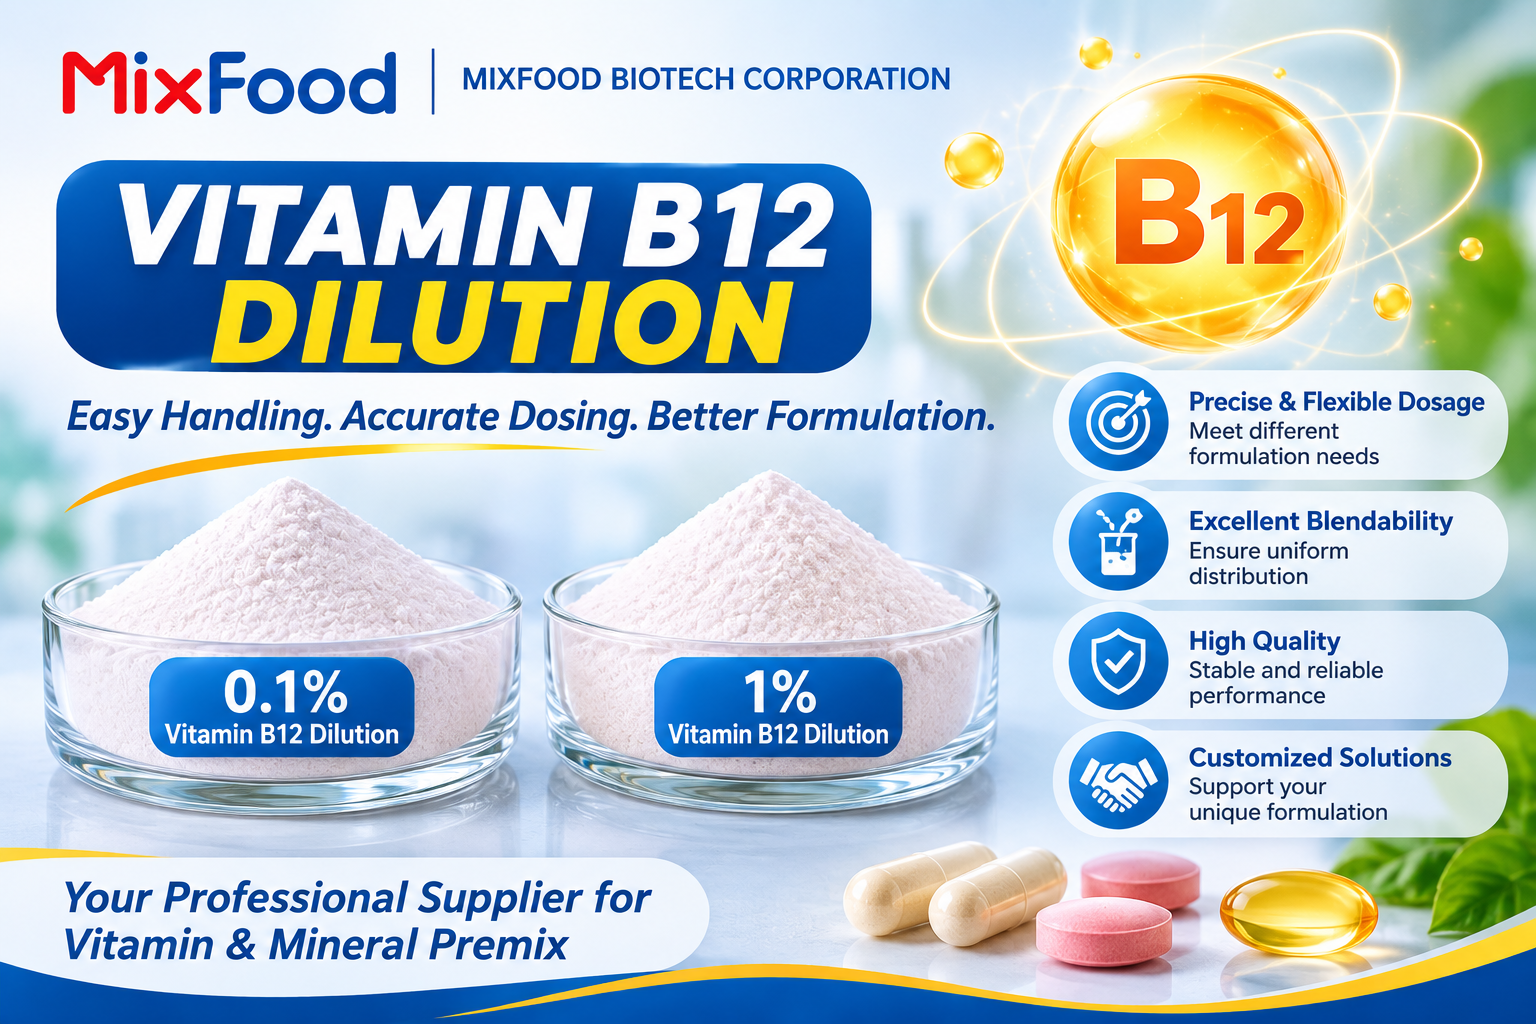
Vitamin B12 is an essential micronutrient widely used in dietary supplements, fortified foods, beverages and multivitamin formulations. However, it is required at relatively low dosage levels compared with many other vitamins and minerals.
Adding a very small quantity of highly concentrated Vitamin B12 directly into a large-scale premix can create challenges in weighing accuracy, uniformity and production handling.
This is why Vitamin B12 dilutions, particularly 0.1% and 1% grades, are commonly considered in vitamin and mineral premix manufacturing.
At MIXFOOD BIOTECH CORPORATION, we provide Vitamin B12 dilution solutions and customized vitamin and mineral premixes designed to meet different formulation and manufacturing requirements.
1. Why Is Vitamin B12 Dilution Important?
Vitamin B12 is used at low inclusion levels in many nutritional formulations. When a highly concentrated ingredient is added in a very small quantity, it can be difficult to distribute evenly throughout a large batch.
Potential challenges include:
• Difficulties in accurately weighing small quantities.
• Risk of uneven distribution during blending.
• Increased sensitivity to differences in production procedures.
• More demanding handling and quality-control requirements.
Using a properly manufactured Vitamin B12 dilution helps make the ingredient easier to handle and incorporate into premix formulations.
The carrier and dilution process should be selected carefully to support the required homogeneity, physical properties and product specifications.
2. Benefits of 0.1% and 1% Vitamin B12 Dilutions
MIXFOOD BIOTECH CORPORATION offers two useful concentration options for different formulation requirements.
0.1% Vitamin B12 Dilution
A 0.1% dilution contains approximately 1 mg of Vitamin B12 per gram of product, subject to the agreed specification.
Key benefits include:
• Lower dosing concentration: Suitable for formulations requiring very low Vitamin B12 inclusion levels.
• Easier weighing: Helps reduce the difficulty of handling extremely small quantities of concentrated Vitamin B12.
• Formulation flexibility: Can be considered for multivitamin and multimineral premixes with specific nutritional targets.
• More convenient blending: Supports the development of formulations where low-dose ingredient distribution requires particular attention.
1% Vitamin B12 Dilution
A 1% dilution contains approximately 10 mg of Vitamin B12 per gram of product, subject to the agreed specification.
Key benefits include:
• Higher concentration: Requires less dilution ingredient than a 0.1% grade to deliver the same amount of Vitamin B12.
• Convenient formulation: Suitable for applications requiring a higher Vitamin B12 contribution.
• Flexible production: Can be incorporated into customized vitamin premix formulations according to dosage and blending requirements.
• Practical handling: Provides an intermediate concentration option between highly concentrated Vitamin B12 and lower-strength dilutions.
3. What Should Manufacturers Consider When Selecting Vitamin B12 Dilutions?
Choosing a suitable dilution involves more than checking the concentration.
Manufacturers should evaluate:
A. Assay and specification: Confirm Vitamin B12 content, test methods and acceptable batch variation.
B. Carrier compatibility: Ensure the carrier is suitable for the intended premix and final product.
C. Blend uniformity: Evaluate particle size, bulk density and physical compatibility with other ingredients.
D. Stability: Vitamin B12 performance should be assessed under the actual conditions of moisture, light, temperature and storage.
E. Application requirements: Consider whether the dilution will be used in tablets, capsules, powders, beverages or other nutritional products.
A suitable dilution grade can support more consistent manufacturing, but uniformity and stability should always be verified through appropriate quality-control testing.
4. MIXFOOD BIOTECH CORPORATION: Your Partner for Vitamin B12 Dilutions and Customized Premixes
MIXFOOD BIOTECH CORPORATION focuses on vitamin and mineral ingredient solutions for nutritional supplement and food fortification applications.
Our product and formulation capabilities include:
• Vitamin B12 0.1% and 1% dilution options.
• Customized vitamin and mineral premixes.
• Ingredient selection based on formulation requirements.
• Consideration of carrier compatibility and blend uniformity.
• Application-oriented formulation support.
• Product specifications and batch quality documentation.
Whether you are manufacturing multivitamin supplements, nutritional powders, fortified foods or other health nutrition products, our team can discuss a suitable Vitamin B12 dilution or customized premix solution based on your requirements.
Conclusion
Vitamin B12 dilution is a practical formulation approach for managing low-dose ingredients in vitamin and mineral premixes.
Both 0.1% and 1% grades offer different advantages in dosage adjustment, handling and formulation flexibility. Selecting the right concentration can help manufacturers simplify ingredient incorporation and support consistent premix production.
Looking for a reliable Vitamin B12 0.1% or 1% supplier, or a customized vitamin and mineral premix manufacturer?
Contact MIXFOOD BIOTECH CORPORATION to discuss your formulation requirements and request product specifications or a quotation.
https://www.mixfoodgroup.com/Vitamins--Minerals-Premix-Solutions.html
MIXFOOD BIOTECH – Your Enjoyable Supplier in Food Ingredients & Nutritional Supplements.
Name: Mixfood Sales
Mobile:86 15221870316
Tel:86 15221870316
Whatsapp:86 15221870316
Email:info@mixfoodgroup.com
Add:Building 1, 385 Yubei Road, Shanghai, China